Progressive Die Stamping
One strip, many stations, a finished part every stroke. The right answer once the annual quantity justifies the tool.
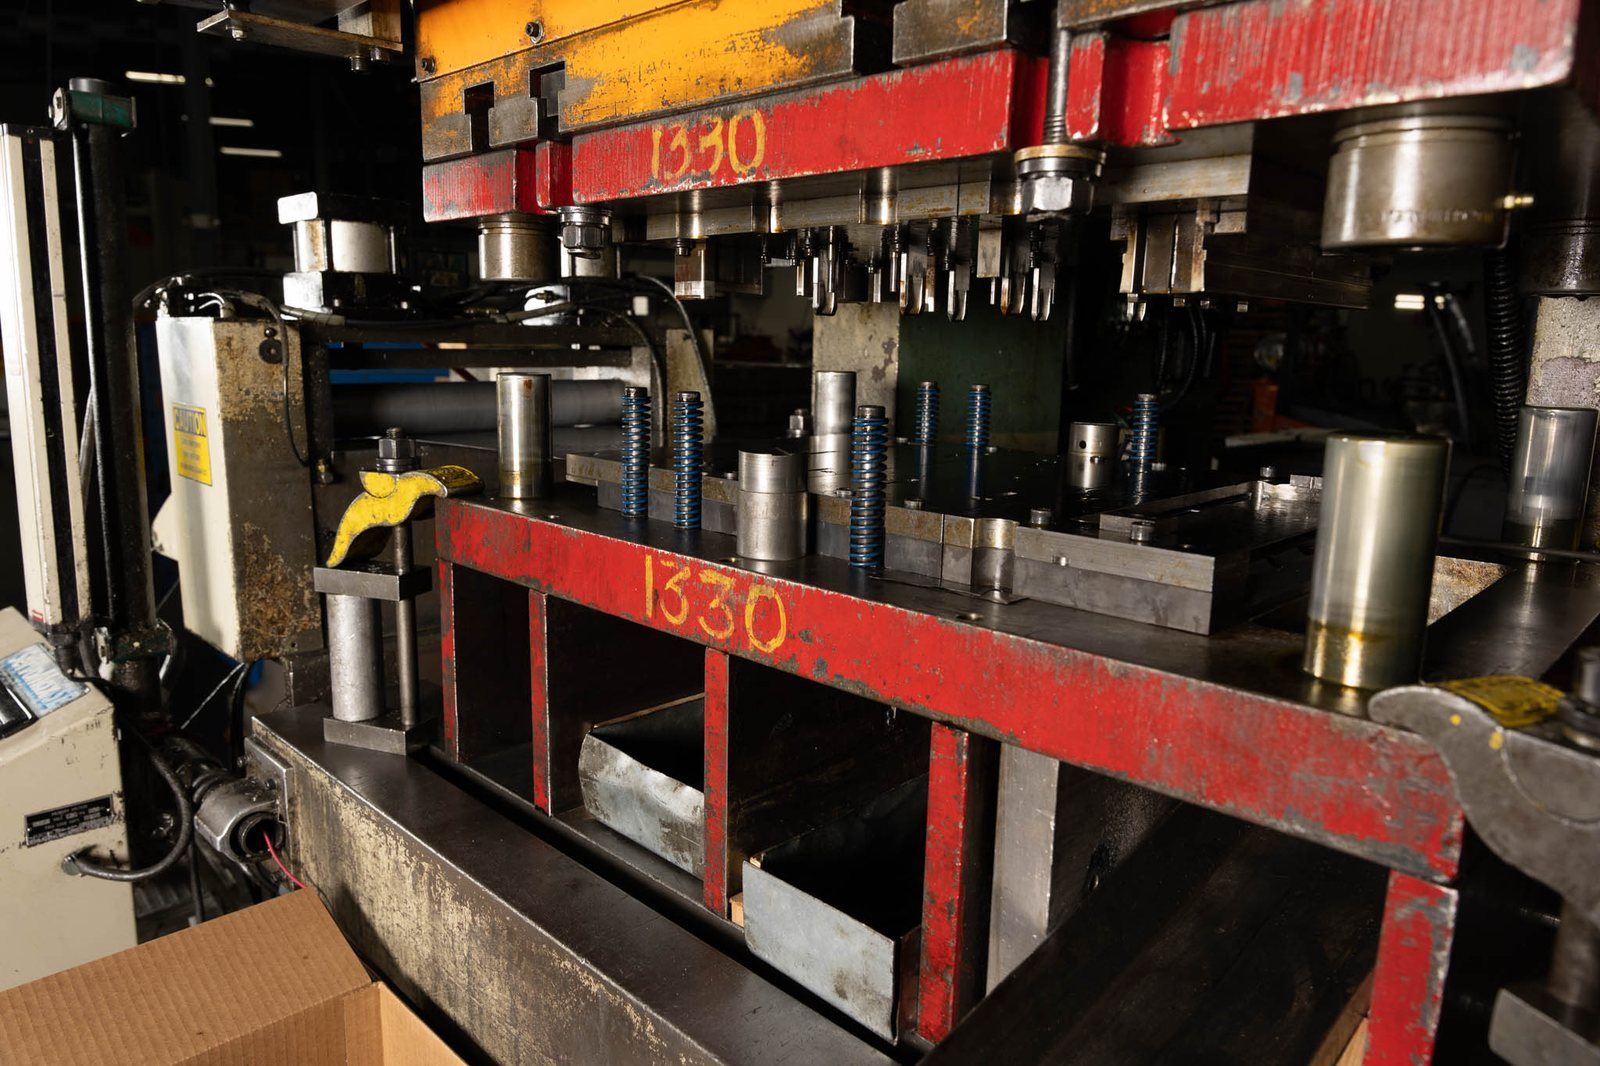
A progressive die does every operation your part needs in one pass. The strip advances one station at a time, each station does one thing, and a finished part drops out at the end of every stroke.
That is why it is cheaper to run than anything else and more expensive to build than anything else. The whole decision is about which of those two facts matters more at your quantity.
What happens inside the tool
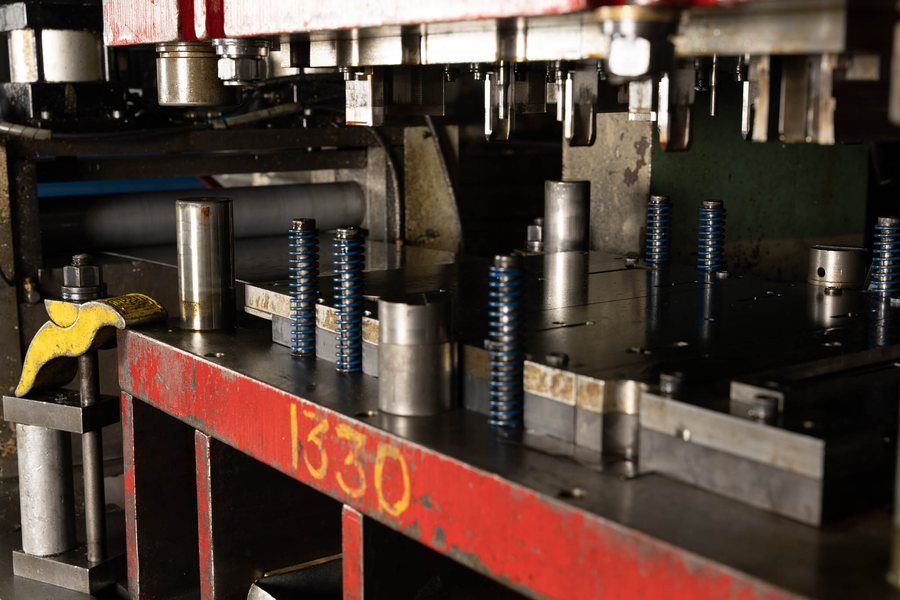
Coil stock feeds in and is pulled through the die by a servo feeder, indexing an exact distance each stroke. Station one might pierce the holes. Station two lances the outline. Further along the strip the part gets bent, flanged, embossed and coined, still attached to a carrier strip that positions it precisely for the next operation. The last station cuts it free.
The part never gets picked up, re-fixtured or re-located between operations, which is exactly why a progressive die holds position so well across a long run. Everything is referenced off the same strip.
When it is the right answer
Usually somewhere around eight thousand parts a year, but the honest answer is that it is a calculation, not a rule of thumb. Take the difference in tooling cost between the two approaches and divide it by the difference in piece price. That is the quantity where the expensive tool becomes the cheaper answer.
Getting it wrong is the most expensive mistake in stamping, in both directions. Build a progressive die for a part that runs two thousand a year and the tooling never pays back. Run a hundred thousand a year off single-hit tooling and you pay for that same die several times over in piece price and setups.
Pay for it once
A progressive die is a real capital decision, which is why what happens afterwards matters. You own one hundred percent of the die set and all related tooling. We store and maintain it for the life of the part at no charge, and you can take it whenever you want.
Setups, maintenance, sharpening, storage and complete rebuilds are covered for as long as the part design does not change and the tool runs on our presses. If it wears out after four million hits, we rebuild it.
Common questions
How many parts justify a progressive die?
Usually around eight thousand a year, but it is a calculation. Divide the extra tooling cost by the saving per part. There is a calculator on our tooling page.
Who owns the die?
You do, one hundred percent, once it is paid for. We store and maintain it at no charge and you can take it whenever you want.
What happens when the die wears out?
We rebuild it at no charge, for as long as the part design has not changed and the tool runs on our presses.
Send us a print
Tell us the part, the material and the annual quantity. We will come back with a straight answer on tooling, lead time and price.
Open Monday through Friday.